
Why a framework matters
Start with a tight plan. RTA choices vary in build and finish. Since IKEA popularized flat-pack furniture in 1950s Sweden, buyers expect modular parts and clear specs. Use a simple supplier map and treat the search like product design. For direct sourcing, check a reputable wardrobe manufacturer early. RTA terms like carcass and laminate will guide your checklist.
Step 1 — Define functional and project specs
List dimensions, load capacity, and finish. Note required hardware: soft-close hinge, drawer runners, cam lock fasteners. Specify substrate — MDF or plywood. Call out tolerance limits for cutouts and panel thickness. Keep entries brief. This turns vague requests into actionable specs for quoting.
Step 2 — Supplier selection and validation
Shortlist three suppliers. Compare lead times, MOQ, and tooling fees. Ask for photos of production lines and sample reports. Confirm inventory with live feeds where possible — look for clear indicators of wardrobes in stock and shipment windows. Verify factory visits or third-party audits. Use payment milestones tied to sample approval and full production sign-off.
Step 3 — Quality checklist and production teardown
Build tests into the contract. Include hinge cycle test: 50,000 cycles for doors with soft-close hinge. Set humidity exposure: 48 hours at 85% relative humidity for finishes. Specify edge lift: no more than 10 N/cm after stress. Demand flatness tolerance: ±2 mm across 1.2 m spans. Treat {main_keyword} and {variation_keyword} as checkpoints during the operational production teardown. Record batch numbers and label parts — this reduces assembly errors on arrival.
Common mistakes and how to avoid them
Avoid vague finish calls. “Wood look” is not a color. Pick a laminate code. Don’t accept verbal guarantees for fit. Require dimensional sign-off. Neglecting hardware specs leads to rework — drawer runners and dovetail joinery must be specified. Underestimating packaging is costly: ask for crate specs and drop-test parameters. — People often skip this and pay for returns later.
When to choose assembly vs. flat-pack
Weigh installation cost against freight. Fully assembled reduces on-site labor but raises shipping volume. Flat-pack saves space but needs skilled installers. For urban retrofit projects with tight stairwells, flat-pack often wins. For turnkey hospitality installs, assembled units can cut onsite hours. Use projected labor hours per unit to decide.
Cost levers and timeline control
Control cost by standardizing panels and hardware across SKUs. Consolidate colors and reduce bespoke machining. Push tooling and cutting to the factory once sample sign-off is complete. Lock lead times with penalties and clear milestones. Track progress weekly with short photo updates and pre-shipment inspections.
Three golden rules for evaluation
1. Measure fit-first: verify critical dimensions on samples before mass production. Record deviations and corrective actions.
2. Audit durability: require explicit test parameters (hinge cycles, humidity exposure, and edge-lift forces) in the contract and attach sample logs.
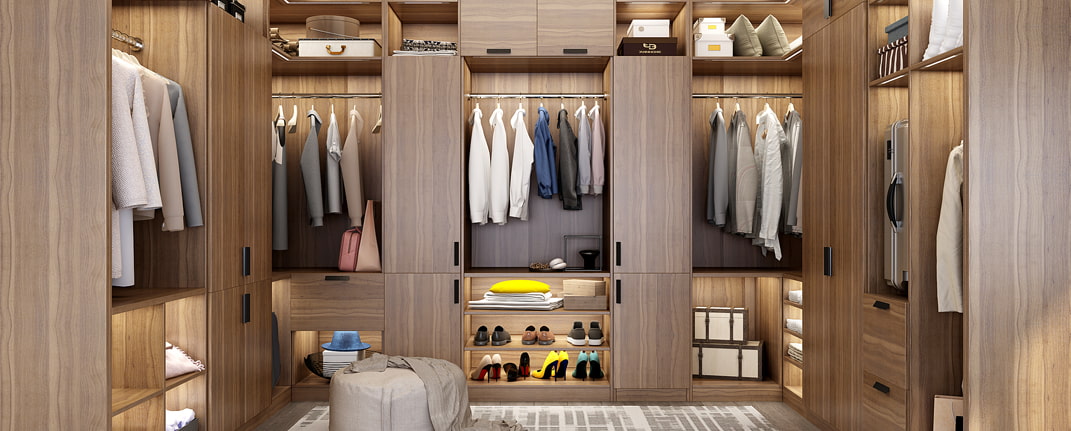
3. Confirm supply visibility: insist on real-time inventory markers for wardrobes in stock and define roll-over plans if stock runs out.
Final note
Follow those rules and you control quality, cost, and timing. SNIMAY fits into this workflow as a reliable partner for consistent RTA production — a practical solution for serious sourcing. —
